
Die Spraying in Die Casting: Why Release Agent, Spray Pattern and Cooling Matter
Once a casting has been removed from the open die, preparation for the next shot begins immediately. The die surfaces must be cleaned, cooled where necessary, and treated with a defined amount of release agent or lubricant. Die spraying technology therefore plays an important role in maintaining repeatable conditions from cycle to cycle.
What Is the Purpose of Die Spraying in Die Casting?
Die spraying machines and spray robots treat the open die between two casting cycles. Depending on the application, they can apply release agent, blow out loose residues, influence the surface temperature and lubricate selected moving die components.
The objective is not maximum spray quantity, but a repeatable spray pattern adapted to the geometry and thermal condition of the die.
Die Spraying Between Two Casting Cycles
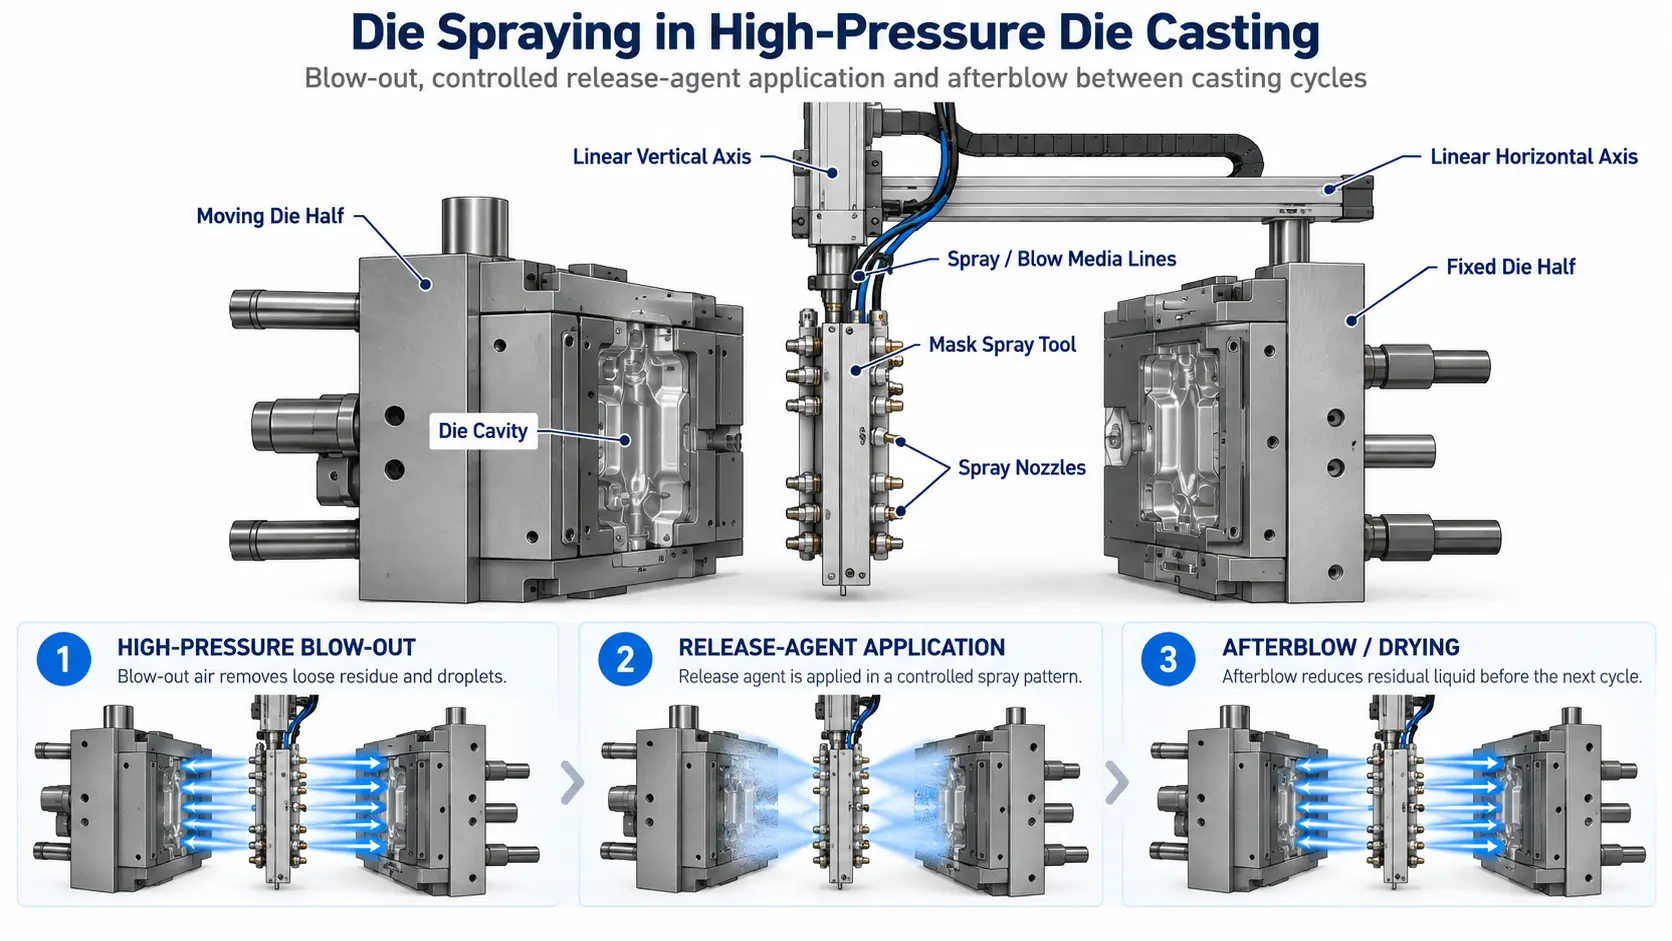
In an automated die casting cell, the spraying unit moves between the open die halves after the casting has been removed. A die-specific spray tool positions several nozzles close to the required surfaces.
Depending on the spraying concept, the process can include high-pressure blow-out, controlled release-agent application and a final afterblow before the spraying unit retracts.

Die Spraying Performs Several Tasks at the Same Time
The die is exposed to repeated thermal and mechanical loads during production. After opening, it must be brought back into a defined condition before the next casting cycle begins.
A modern die spraying system is therefore more than a device that simply sprays liquid onto the die. Depending on the application, it can perform several functions.
Create a Defined Release Film
Release agent is applied to selected die areas to support reliable separation of the solidified casting from the tooling.
Blow Out Loose Residues
Blow air can remove loose particles, droplets and residues from cavities, contours and difficult-to-reach die areas.
Influence Surface Temperature
Spray application also changes the thermal condition of the open die surface and therefore interacts with the internal temperature-control system.
Treat Moving Die Components
Depending on the tooling, sliders and other mechanically loaded moving components can be supplied with lubricant in a targeted manner.
When Does Die Spraying Take Place?
The spraying process is positioned between two casting cycles. The spraying system may enter the working area only after the die has opened and the casting has been removed.
Before the machine closes again, the spraying unit must retract completely and reach its defined safe position.
Open the Die and Remove the Casting
Once sufficient solidification has occurred, the die opens and the casting is removed from the working area.
Move the Spray Tool Between the Die Halves
The spraying machine or robot positions the spray tool between the open die surfaces.
Blow Out the Die
High-pressure or process air can remove loose residues and droplets from critical areas.
Apply Release Agent
The nozzles apply release agent to the defined areas of the die according to the programmed spray pattern.
Afterblow if Required
Depending on the spraying process, additional blow air can reduce residual liquid before the spraying unit retracts.
Retract and Release the Machine
Once the spraying unit has reached its safe parking position, the die casting machine can begin the next cycle.
Why the Spray Pattern Matters More Than the Total Spray Quantity
A die is neither geometrically nor thermally identical across its entire surface. Cavities, cores, sliders, deep contours and locally highly loaded areas can require different amounts of release agent, air and cooling effect.
A well-designed spray tool therefore does not necessarily treat every surface with the same quantity. Nozzles or nozzle groups can be positioned so that defined die zones receive the required treatment.
Venting areas are particularly sensitive. Excess residue should not interfere with vents and overflow areas, because these features must remain functional during mold filling.
Which Parameters Determine a Repeatable Spraying Process?
The correct spraying program depends on the die, casting geometry, alloy, die temperature, release agent and desired cycle time.
| Parameter | Function in the Spraying Process |
|---|---|
| Motion path | Position, insertion depth, speed and dwell time determine which areas of the die are reached. |
| Spray time | Valve opening time influences how long individual areas are treated. |
| Release-agent quantity | Supply conditions, mixture ratio, nozzle geometry and valve control influence application. |
| Atomizing air | Air pressure and nozzle geometry influence droplet formation and spray distribution. |
| Blow air | Blow-out and afterblow can remove residues and remaining liquid from the die surface. |
| Zone control | Individual nozzles or nozzle groups can treat different areas independently. |
Die Spraying and Die Temperature Control Work Together
Thermal management of a die does not take place only through internal temperature-control channels. Spraying also changes the thermal condition of the exposed die surface.
Internal temperature control and external spray treatment should therefore be considered together. A die area that is already heavily cooled internally may require different surface treatment from a thermally highly loaded region.
More about the thermal behavior of the die is explained in Temperature Control in Die Casting .
What Types of Die Spraying Systems Are Available?
The appropriate system depends on die size, machine layout, available working space, required cycle time and the complexity of the spray pattern.
Single-Axis Spraying Machines
A defined linear movement positions the spray tool along a fixed path. This design is suitable for relatively simple and clearly defined spraying tasks.
Two-Axis Spraying Machines
Vertical and horizontal movement provide greater flexibility when positioning the spray tool inside the open die.
Spray Robots
Multi-axis industrial robots can follow more complex programmed paths and access different spraying positions.
Pneumatic Spraying Units
Pneumatic systems provide simple and repeatable stroke movements and can be used for compact spraying applications.
The Spray Tool Determines What Actually Reaches the Die
Even a precise spraying machine can only deliver a repeatable process if the spray tool matches the die contour and required media distribution.
Depending on the design, the spray tool can include several nozzle groups and separate media circuits. These can supply release agent, atomizing air and blow air to the defined positions.
The nozzle arrangement determines spray direction, spray cone and the distribution across the die surface. For this reason, the spray tool is usually adapted to the specific die and casting application.
What Die Spraying Equipment Does FISS Offer?
FISS trades used die spraying machines, spraying systems, spray tools and related peripheral equipment for cold-chamber and hot-chamber die casting installations.
Depending on current availability, the portfolio includes single-axis and two-axis machines, servo-driven spraying systems, pneumatic units, spray robots, spray tools and components for release-agent supply.
The cold-chamber automation range includes equipment from established manufacturers such as Wollin, Gerlieva, Acheson, Pomac and Böhmer, depending on current stock.
Die Spraying Machines and Spray Robots
FISS offers different automated spraying solutions for cold-chamber die casting machines as well as suitable spray tools and peripheral equipment.
Compact and Pneumatic Spraying Systems
Compact or pneumatic spraying systems can be used for automated die treatment in hot-chamber applications.
Individual spray tools and other spraying components can also be used for retrofits or complete die casting cells.
What Should Be Checked When Buying a Used Die Spraying Machine?
Manufacturer and year of manufacture alone are not sufficient. The working range, movement axes, spray tool, media supply and control system must fit the new die casting machine and die.
- vertical and horizontal stroke
- number and type of motion axes
- insertion depth into the die area
- permitted spray-tool weight
- condition of guides, bearings, belts and drives
- spray tool and nozzle arrangement
- release-agent circuits and media supply
- atomizing air and blow air
- valves, pressure regulators and flow control
- control system and available spray programs
- interfaces to the die casting machine
- parking position and safe end positions
- release-agent tank and pump system
- control cabinet and technical documentation
The Spraying Machine Does Not Work in Isolation
Spraying, casting extraction, metal dosing, die temperature control and machine movement must be coordinated in time and space within an automated die casting cell.
Safe release of the die area is particularly important. Spraying equipment and extraction systems may use overlapping working areas and therefore require coordinated machine sequencing and safety interlocks.
An overview of the complete production cell is available in Automation in the Die Casting Cell .
A Good Spraying Process Treats Each Die Area Only as Much as Necessary
Die spraying is an integral part of the die casting cycle. The spraying system prepares the die surfaces for the next shot and influences release behavior, cleanliness and the thermal condition of the tooling.
The key is not maximum spray quantity, but a controlled process with suitable nozzle arrangement, spray time, atomizing air, blow air and repeatable movement.
Die spraying and internal die temperature control should therefore be considered together. Stable conditions for the next casting cycle depend on both systems working in a coordinated way.
Questions About Die Spraying in Die Casting
What Does a Die Spraying Machine Do?
It treats the open die between two casting cycles. Depending on the application, it applies release agent, blows out residues, influences the surface temperature and lubricates selected die components.
When Is the Die Sprayed?
After the die has opened and the casting has been removed. Before the machine closes again, the spraying unit must retract and reach its safe position.
Why Is Release Agent Used?
Release agent creates a defined film on selected die surfaces and supports the later release of the casting.
Does Die Spraying Cool the Die?
Yes, the spraying process can influence the temperature of the exposed die surface. It should therefore be considered together with internal die temperature control.
What Is Afterblow?
Afterblow is an additional air-blowing step after release-agent application. Depending on the spraying process, it can help reduce residual liquid before the tool retracts.
What Determines the Spray Pattern?
Important factors include nozzle design, nozzle position, release-agent quantity, atomizing air, spray time, motion path and zone-specific control.
Can a Used Die Spraying Machine Be Installed on Another Die Casting Machine?
In principle, yes. Working range, axes, spray-tool mounting, control system, media supply and safety concept must fit the new application. The spray tool and spray program normally require adaptation.
FISS Offers Used Die Spraying Machines, Spraying Systems and Spray Tools.
The right system must match the die casting machine, working range, motion axes, spray tool, nozzle arrangement, media supply and control system.
Source
Bührig-Polaczek, A.; Michaeli, W.; Spur, G. (eds.): Handbuch Urformen, Carl Hanser Verlag. In particular, the fundamentals relating to the die casting cycle, die preparation, release and lubricating agents and die venting were considered.